
Seamless Rolled Rings & Forgings
Custom drawing-based forged rings up to 500mm OD developed inside a rapid 15-day tooling loop.
500mm OD
Max Ring Rolling
In-house
Tooling Shops
GNR Italy
Spectrometer Lab
Where Our Components Work
Precision engineering configurations designed for severe service environments in the Heavy Engineering Solutions market.
Wind Turbine Pitch Rings
Planetary pitch ring gear blanks to rotate windmill blades.
Heavy Gearbox Blanks
Large rings rolled to minimize scrap weights during gear teeth cutting.
Thick Spacer Sleeves
Seamless cylinder sleeve sleeves designed to hold heavy axle loads.
Customized Forged Blocks
Heavy closed die structural forgings for industrial turbines.
Relevant Products Used
OEM drawing-based components manufactured from certified raw steel with uniform grain boundaries.

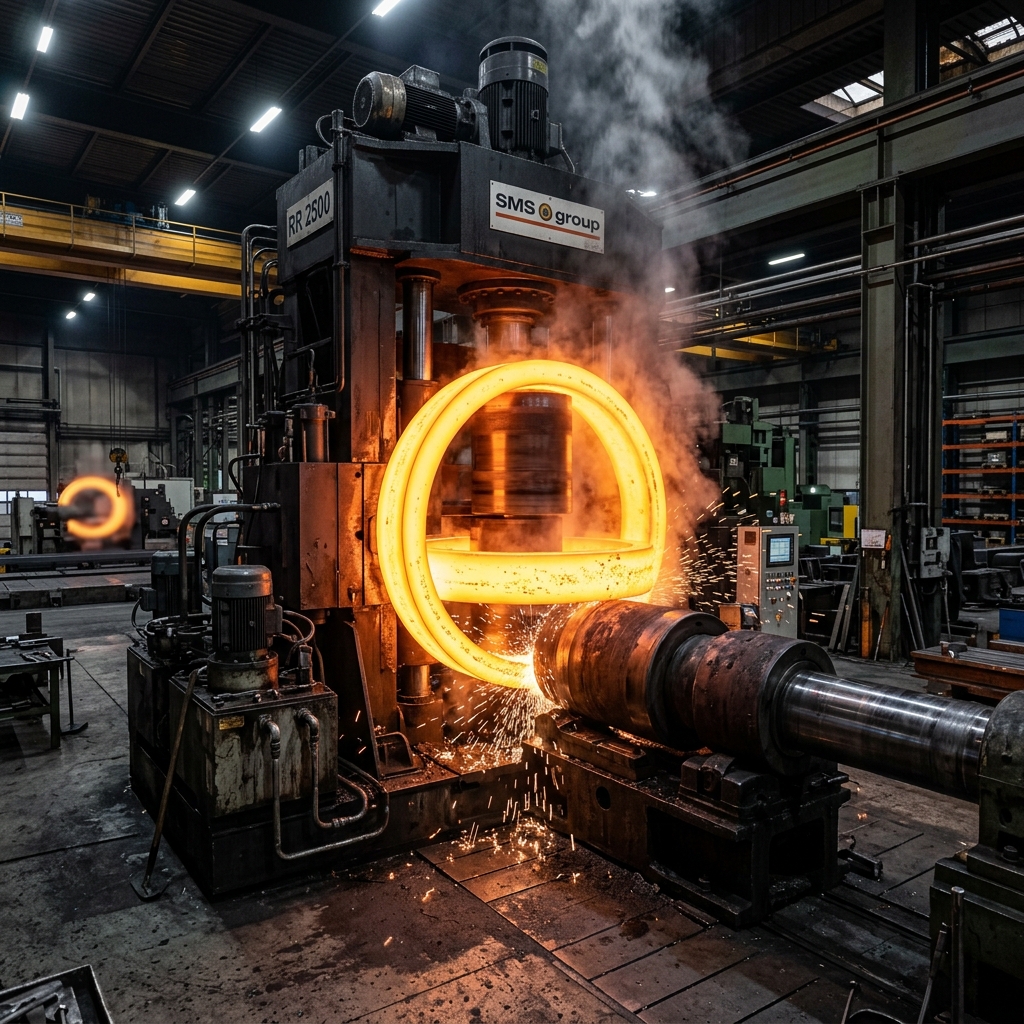
Seamless Rolled Rings
Seamless rolled ring blanks. Radial-axial rolling ensures no grain breaks.
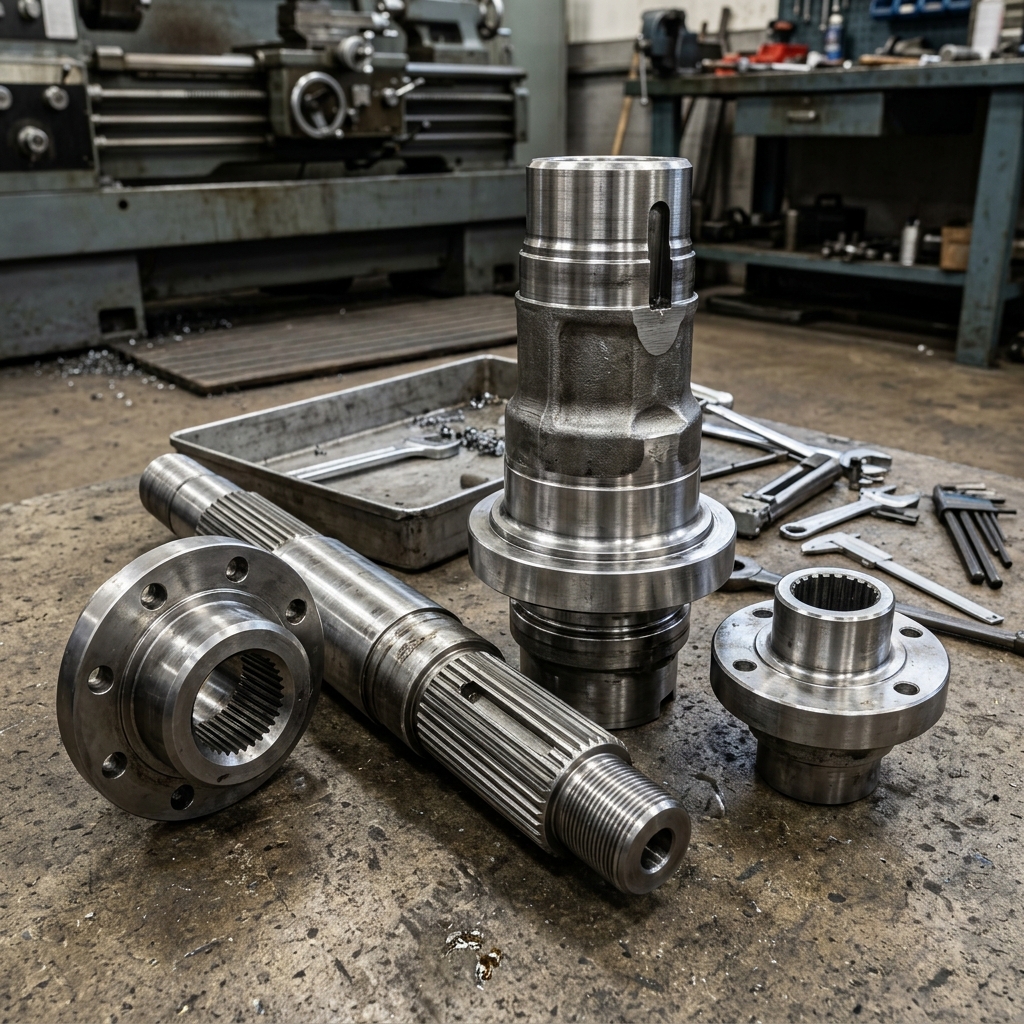
Large Spacer sleeves
Seamless tubes punched and rolled. Rough turned to customer specs.
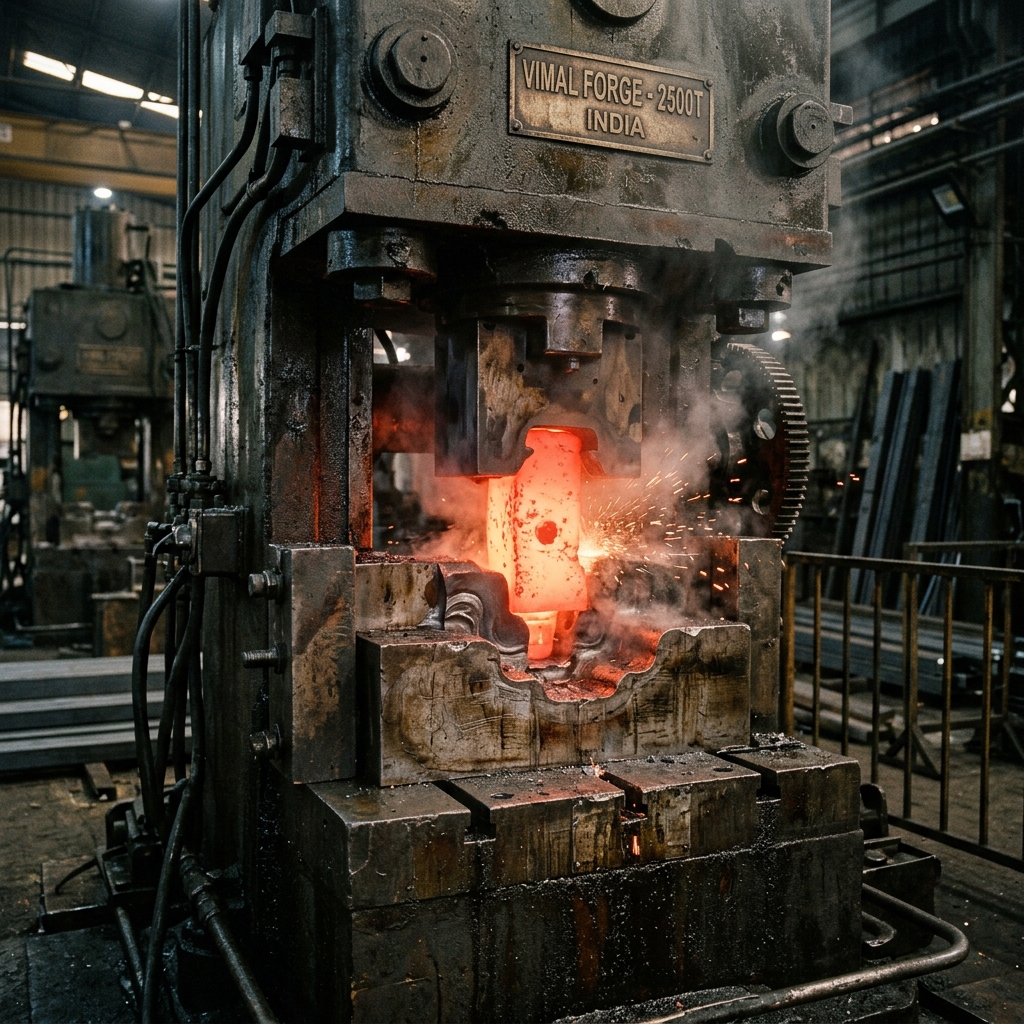
Customized Die Forgings
Heavy closed-die components machined with custom tool layouts.
Material Grade Matrix
Alloy grades heat treated to match client specifications for ultimate tensile yield and fatigue defense.
Alloy Detail Panel
---
---
---
---
Capabilities & Workflow Used
How we carve dies, forge billets, and turn components to ensure fully dense structures.
Radial-Axial Ring Rolling
High dimensional reproducibility for gear ring blanks up to 500mm OD.
In-house Die shops
Dies carved inside a 15-day development loop for custom drawings.
NDT QA Inspection
100% MPI crack testing and Italy spectrometer checks ensure zero defect shipments.
Machinery & Product Gallery
Unretouched B2B photographs showing actual products, CNC lathe lines, and hammer presses.
Quality Assurance & Material Traceability
We protect B2B client integrity using certified spectrometer inspection and heat-code barcoding audits.
Spectrometer Chemistry
GNR Italy optical emission spectrometers check alloy contents. Zero billing is approved without chemical conformity logs.
100% MPI Crack Audits
Magnetic particle inspection (MPI) filters out any micro-voids, boundary folds, or internal fissures on high-stress components.
Heat Code laser stamping
Each component receives a laser-stamped batch heat number, linking raw material chemical certificates to the final product shipment.