
Our Manufacturing Process
Converting certified steel billets into high-precision, fully finished OEM components through our integrated 10-step value chain.
Physical Progression Journey
See how we transform raw steel into high-precision finished components using our integrated operations.
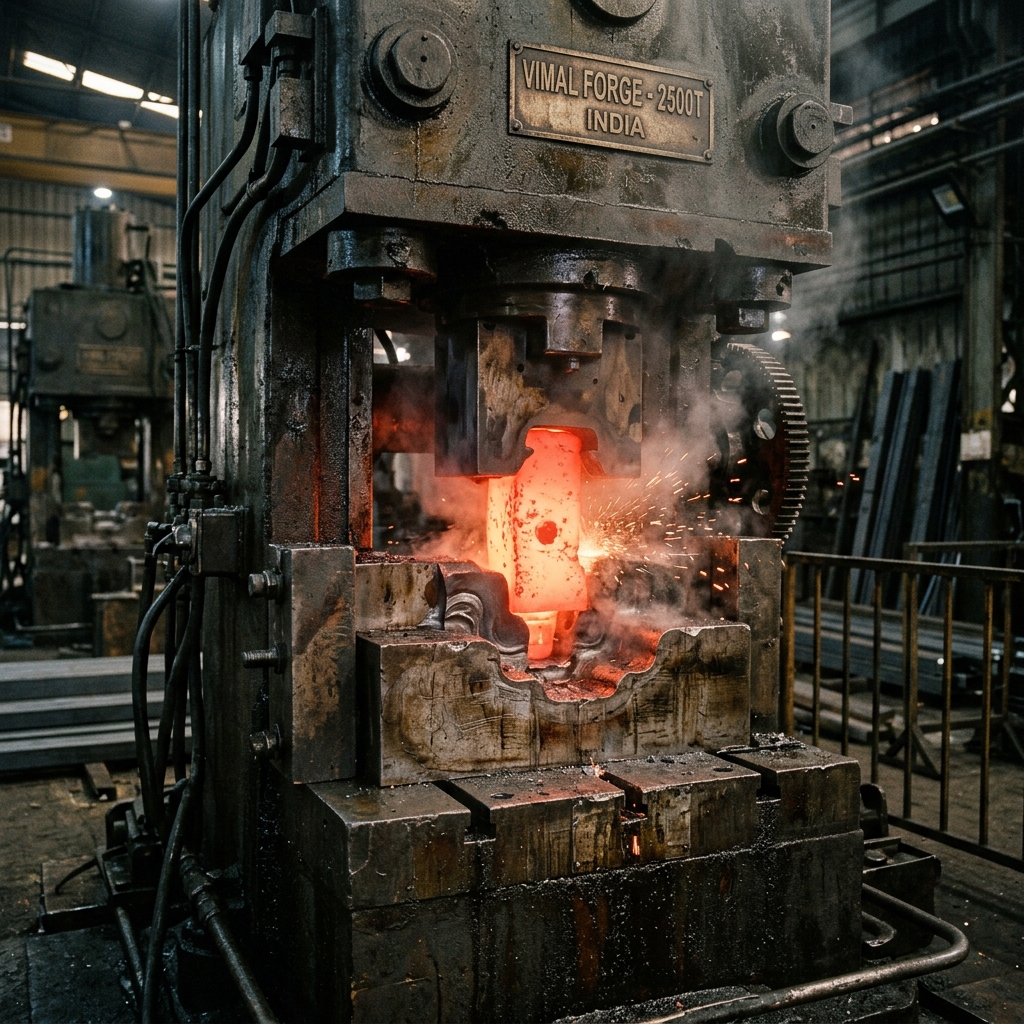
1. Raw Material
Certified alloy steel bars sourced from approved prime mills, color coded and chemical spectro tested.
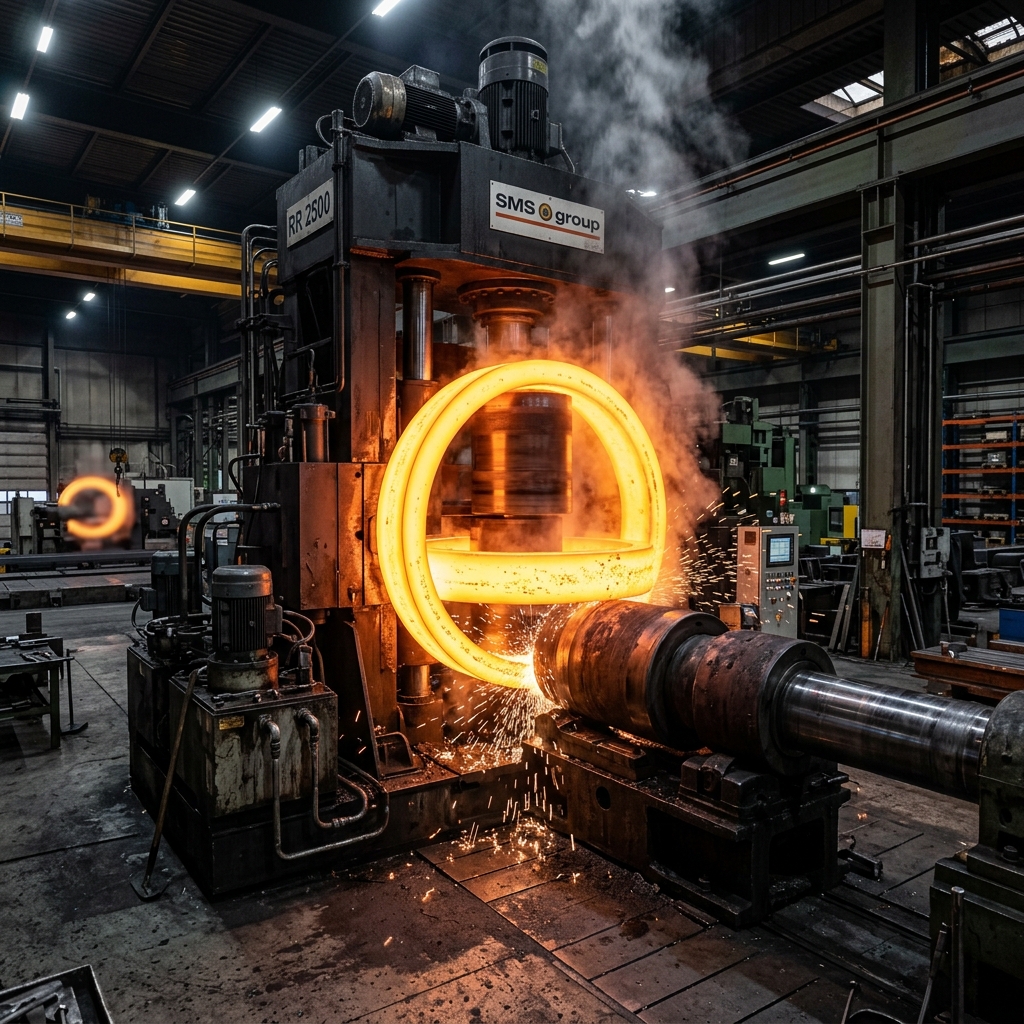
2. Forged Component
Hot forged drop parts or CNC rolled rings with seamless grain layout orientation for high stress loads.
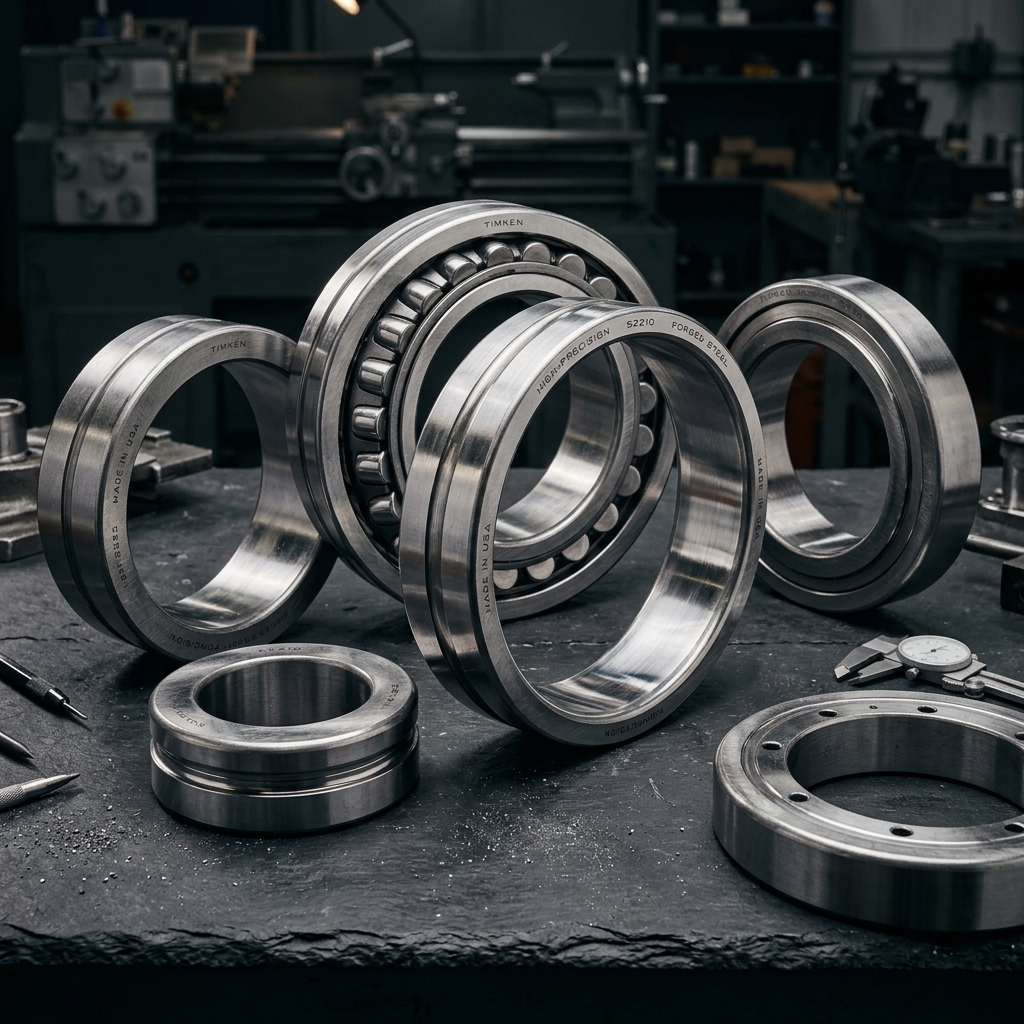
3. Machined Component
Finish-turned on CNC lathes and slotted on vertical VMCs. Critical seating dimensions ground within +/-10μm.
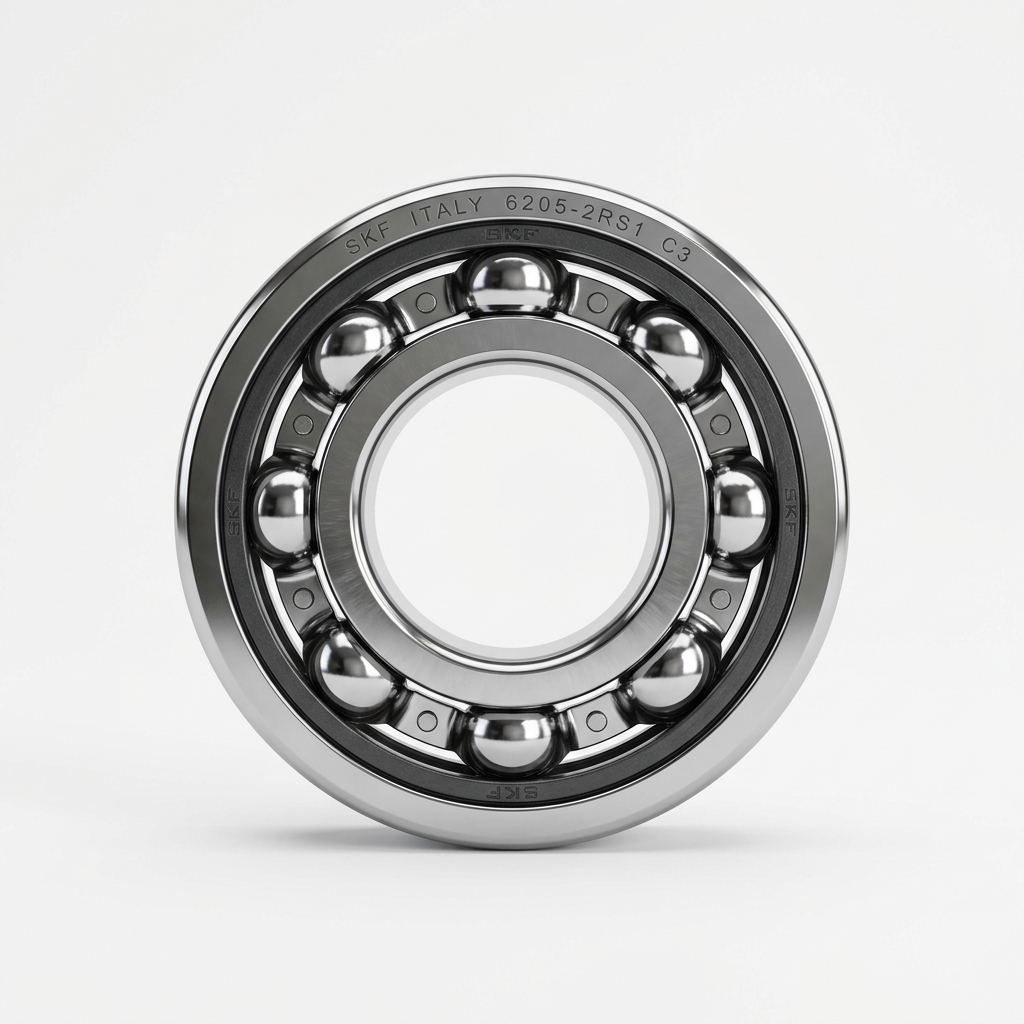
4. Finished Product
Laser heat-coded, NDT inspected, oil dipped, and sealed inside VCI moisture-barrier bags on wood pallets.
10-Step Value Chain
Raw Material Sourcing & Spectro Check
Procured only from approved prime steel mills. Billets are chemical spectro checked upon arrival to match Mill Test Certificates (MTC) exactly.
Billet Shearing & Cutting
Billets are cut to calculated weights via circular and band saws. Consistent weights minimize material flash loss and maximize yield values.
Induction Billet Heating
Induction heating maintains a uniform temperature throughout the steel preforms, preventing scale formation and internal thermal micro-cracks.
Closed Die Forging
Billets are drop-forged inside detailed tool rooms die cavities. Establishes structural grain flows required for high stress applications.
CNC Ring Rolling
Preforms are punched and expanded on automatic radial-axial CNC ring rolling mills to exact outer diameters and wall thicknesses.
Controlled Heat Treatment
Uniform heating and slow cooling curves (spheroidized annealing) eliminate internal stress and optimize machinability limits.
Precision Machining (CNC & VMC)
Finish turning on turning centers, and milling slot alignments on VMCs. Bearings seating faces ground within 10 microns limit.
Quality Inspection & NDT Testing
Hairline cracks checks using wet MPI, and sub-surface validation using Ultrasonic waves. Unique heat numbers laser marks components.
Rust Prevention & VCI Packaging
Dipped inside premium anti-rust oil, bagged with Volatile Corrosion Inhibitors (VCI), and packed onto heat-treated pallets.
Logistics & Dispatch
Trucked directly to Gujarat ports (Mundra/Pipavav) and loaded into cargo ships along with Mill Test Certs (MTR) and dimensional layouts.